Manufacturing
Work-in-process, tools, quality gates and line-side material.
01 / THE QUESTION
Where does
visibility break?
Work-in-process, tools, quality gates and line-side material. RFID becomes valuable when it reduces a specific handoff, search, count or verification problem and puts a trusted event into the right system.
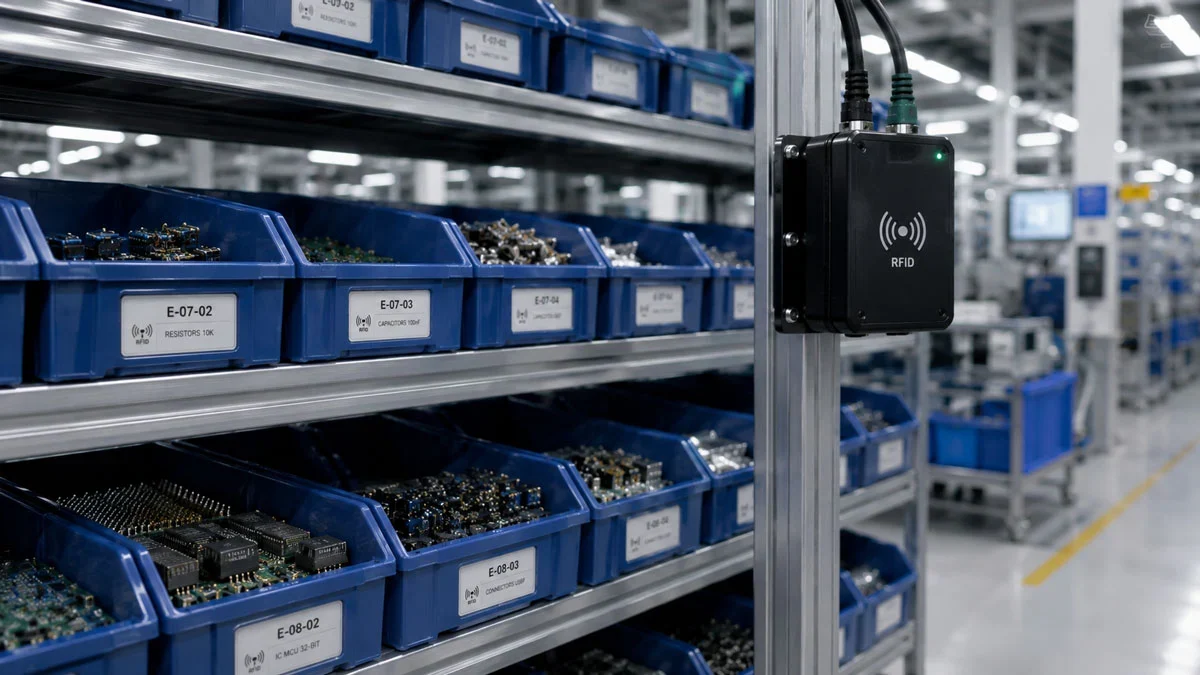
FIELD VIEW / COMPONENT FLOW
Keep parts
in the right sequence.
Manufacturing RFID can connect work-in-process, tools and line-side material when attachment and event rules are proven on representative items.
- Identify work-in-process, kits or tools at defined stations
- Capture movement and quality-gate events in sequence
- Test attachment, orientation and interference on real items
02 / INDUSTRY WORKFLOW
Four moments.
One accountable handoff.
Connect material, work order and station events without relying on paper travelers. The sequence below is specific to the operating environment and remains subject to representative testing.
Identify the work unit
Tie a container, kit, work order or tool to the station context that will own the next transition.
Confirm station arrival
Check that the expected unit reached the station or buffer instead of treating every nearby observation as process completion.
Apply the process rule
Validate sequence, quality hold and material conditions before allowing the next state to be posted.
Escalate the hold
Make missing, wrong or out-of-sequence material visible to the operator and the process owner.
03 / INDUSTRY KIT
Equipment follows
the operating point.
A starting configuration for this industry may include these elements. The exact model, tag construction, region and availability remain project questions.
04 / INDUSTRY-SPECIFIC SCOPE
Make the material
and risk explicit.
Industry context changes the test. These are the details to carry into the first sample, site survey or proof of concept.
Read the planning guideWork-in-process, kits, line-side containers, tools and station states.
Metal, liquids, sequence changes and a raw read being mistaken for process completion.
Test one station transition with expected, missing and out-of-sequence items and its MES/ERP response.
05 / SYSTEM HANDOFF
Respect the
system of record.
Manufacturing integration should carry work context, station, state and hold reason to MES or ERP without turning raw reads into automatic completion.
06 / DEPLOYMENT PATH
Prove one
repeatable moment.
Map the process, define event ownership, pilot one route, document recovery paths and then expand by line or product family.
- Define the acceptance target
- Test the item and environment
- Train the people who own the exception
- Scale only after the workflow is usable
07 / INDUSTRY FAQ
Scope the first
conversation.
Some can, but construction and attachment are application-specific. We test temperature, chemicals, abrasion and re-use before making a recommendation.
Yes. The middleware or MES layer can compare the EPC and station event with the expected route and create an exception when they differ.